THS16R: Where Speed, Temperature, and Flexibility Converge on the Laboratory Bench.
Efficiency is not merely about the speed at which a process can be completed. More importantly, it is defined by an instrument's ability to maintain sample quality and process consistency while adapting to diverse analytical needs. Welcome to the world of the modern laboratory!
The centrifuge is a crucial piece of equipment in this workflow. Whether for cell separation, bacterial isolation, plasmid extraction, or protein purification, the centrifugation process requires a combination of speed, centrifugal force, temperature control, and operational stability. Laboratory needs are becoming increasingly diverse; a single laboratory might handle samples in microtubes for one process and then switch to 15 ml or even 50 ml tubes for the next. Relying on multiple centrifuges to meet these requirements inevitably increases space requirements, equipment investment costs, and operational complexity.
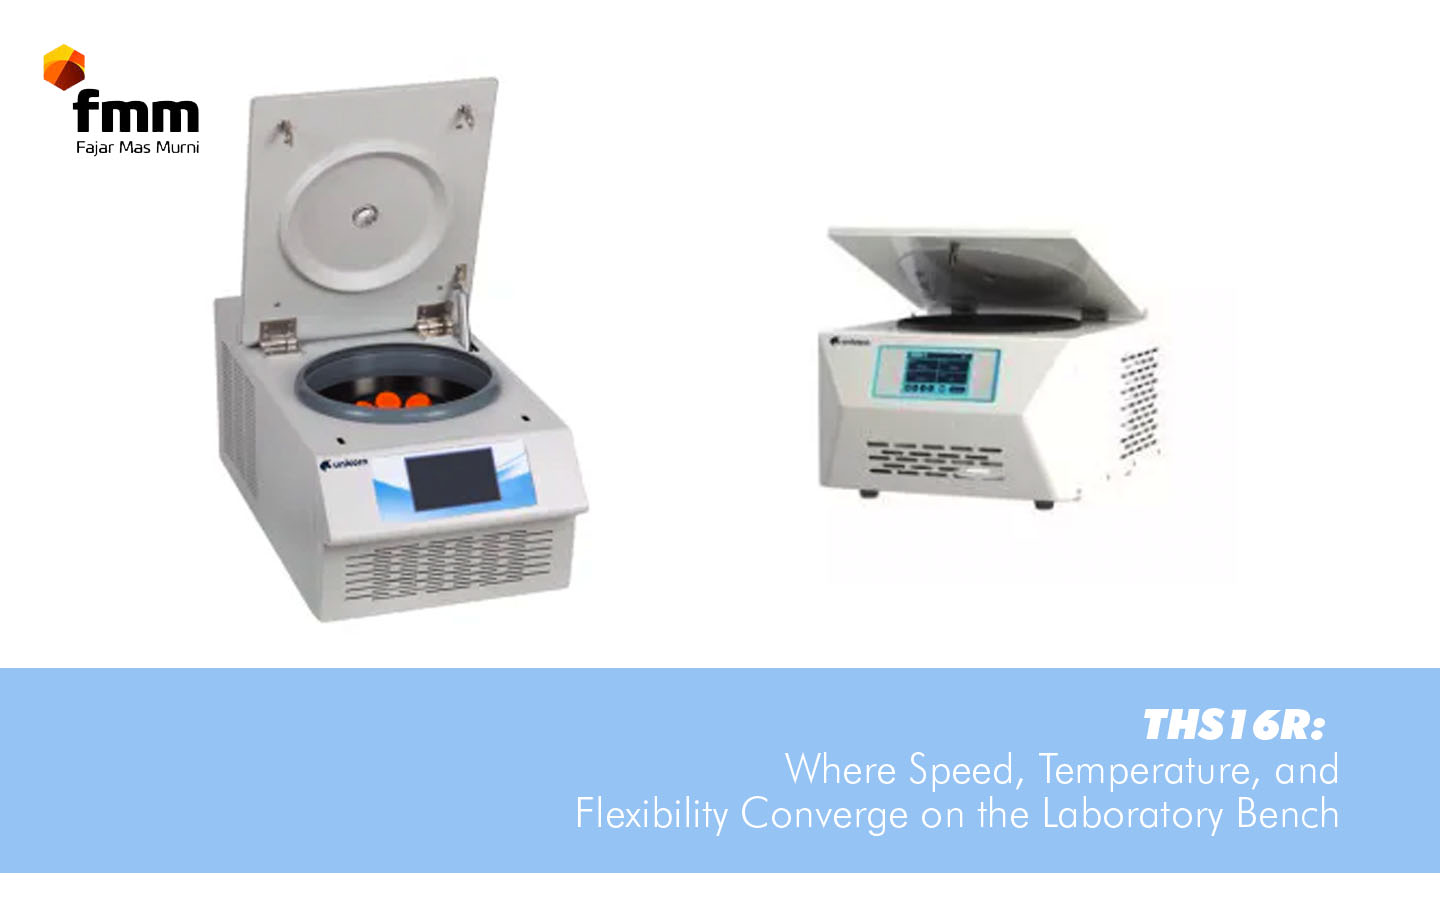
This is where the Unicorn Lifescience THS16R Tabletop Compact High-Speed Refrigerated Centrifuge offers a different approach: delivering the performance of a high-speed refrigerated centrifuge within a design that remains compact and efficient for laboratory benchtop use.
The THS16R is more than just a high-speed centrifuge; it is designed to meet specific operational needs by combining high-speed performance, refrigerated operation, and flexible rotor options. With a capacity of up to 6 × 50 ml, the device accommodates processes requiring larger sample volumes while supporting various rotor configurations for microtubes as well as 5 ml, 10 ml, and 15 ml tubes. Consequently, a single unit can support multiple stages of laboratory workflows without compromising valuable workspace.
Maintaining sample stability at high speeds.
In various molecular biology and protein chemistry applications, temperature is not merely an additional parameter. Temperature fluctuations can affect the stability of proteins, enzymes, and specific biological components. The THS16R features a cooling system capable of maintaining the chamber temperature at 4°C during maximum-speed operation. Notably, the rapid pre-cooling function allows the chamber temperature to drop from approximately 25°C to 4°C in about six minutes.
This capability offers a practical advantage for laboratories handling temperature-sensitive materials. Pre-processing wait times can be reduced, while temperature conditions can be tightly controlled from the very start of the centrifugation process. The THS16R features a temperature setting range of -20°C to 40°C, with a temperature accuracy of ±1.0°C.
High performance does not necessarily require bulky equipment. The THS16R measures approximately 620 × 327 × 270 mm and has a net weight of 40 kg. This design allows the unit to be placed on a workbench without occupying the vast amount of space required by large-capacity centrifuges. For laboratories with limited space, this compact design offers a distinct advantage, enabling optimal use of the workspace while still meeting high-speed, refrigerated centrifugation needs. In terms of performance, the THS16R achieves a maximum speed of 16,500 rpm and a maximum Relative Centrifugal Force (RCF) of up to 22,380 × g, making it ideal for applications requiring high centrifugal force within a tabletop format.
The THS16R supports a variety of fixed-angle rotors, ranging from:
12 × 1,5/2 ml
24 × 1,5/2 ml
36 × 1,5/2 ml
18 × 5 ml
12 × 10 ml
12 × 15 ml
6 × 50 ml
With this range of options, the THS16R can be utilized across various stages of the laboratory workflow, from micro-volume applications to sample processing in 50 ml tubes. This flexibility is particularly valuable when laboratories aim to optimize their instrument investment; instead of maintaining separate units for different tube sizes, a single platform can be configured to meet specific process requirements.
High-speed operation is matched by a comparable safety system. The THS16R utilizes high-strength steel construction and features an Automatic Rotor Identification system; this system ensures correct rotor identification and limits operating speed according to the rotor's specific capabilities. Protection against imbalance is also integral to the safety system, which incorporates a three-stage shock absorption system, automatic balancing, and an auto-shutdown function triggered by imbalance. Through this approach, safety is not treated as a mere add-on feature but is instead embedded in the instrument's overall design.
Modern laboratories require instruments that are not only powerful but also user-friendly. The THS16R features a 5-inch interactive touchscreen that allows operators to set and monitor parameters such as speed, centrifugal force, time, and temperature. These parameters can be adjusted in real-time without stopping the machine. For repetitive tasks, the device can store up to 99 customizable programs; this feature reduces the need for manual setup and enhances consistency when performing the same procedure repeatedly. The THS16R also offers 10 levels of acceleration and deceleration settings, as well as soft start/stop functionality, helping to minimize the risk of sample remixing during the centrifuge's deceleration phase.
Combining speed, cooling capabilities, and rotor versatility, the THS16R is designed to meet a wide range of laboratory needs, particularly in the fields of molecular biology and protein chemistry. Supported applications include:
Bacterial Isolation: A capacity of up to 6 × 50 ml enables the pelleting of bacterial cultures in larger volumes.
Plasmid Extraction: The microtube configuration supports DNA preparation and processing steps involving small volumes.
Protein Purification: High-speed centrifugation and refrigerated operation capabilities facilitate processes requiring both high centrifugal force and temperature control.
Sample Processing: Support for 5 ml, 10 ml, 15 ml, and up to 50 ml rotors provides flexibility in handling various sample volumes.
Unicorn Lifescience positions the THS16R as a solution for laboratories that need the ability to switch between microtubes and 50 ml tubes without having to operate two separate centrifuge units.
The needs of each laboratory may differ. Yet one requirement is becoming increasingly universal: an instrument must be able to deliver reliability, flexibility, efficiency, and control within a single system. The THS16R addresses this need through a combination of:
- Maximum speed up to 16,500 rpm
- Maximum RCF up to 22,380 × g
- Refrigerated operation with a temperature range of -20°C to 40°C
- Rapid pre-cooling to 4°C in approximately 6 minutes
- Capacity up to 6 × 50 ml
- Wide range of rotor options for various tube sizes
- Automatic rotor identification
- Automatic balancing and unbalance protection
- 5-inch touchscreen
- Storage for up to 99 programs
- Compact tabletop design
For laboratories requiring a centrifuge with broad capabilities while also prioritizing space and workflow efficiency, the THS16R offers an attractive proposition.
For PT Fajar Mas Murni (FMM), supplying laboratory equipment goes beyond merely providing a product. More importantly, it involves understanding user needs and helping to select solutions that align with workflows, applications, and operational demands in the field. Through its laboratory instrumentation solutions, FMM is committed to partnering with various industries—ranging from research laboratories, pharmaceuticals, and food & beverage to manufacturing and other sectors requiring reliable analysis and quality control processes.
The THS16R serves as an example of how centrifugation technology can be designed to meet the needs of modern laboratories: faster, more flexible, and offering greater control, all while remaining space-efficient.
Because ultimately, a good laboratory instrument is not merely one with high specifications, but one that enables the entire workflow to function more effectively.
Administrator System
